Rack Contact Design for Stable Current Distribution in Electroplating
2026-09-23
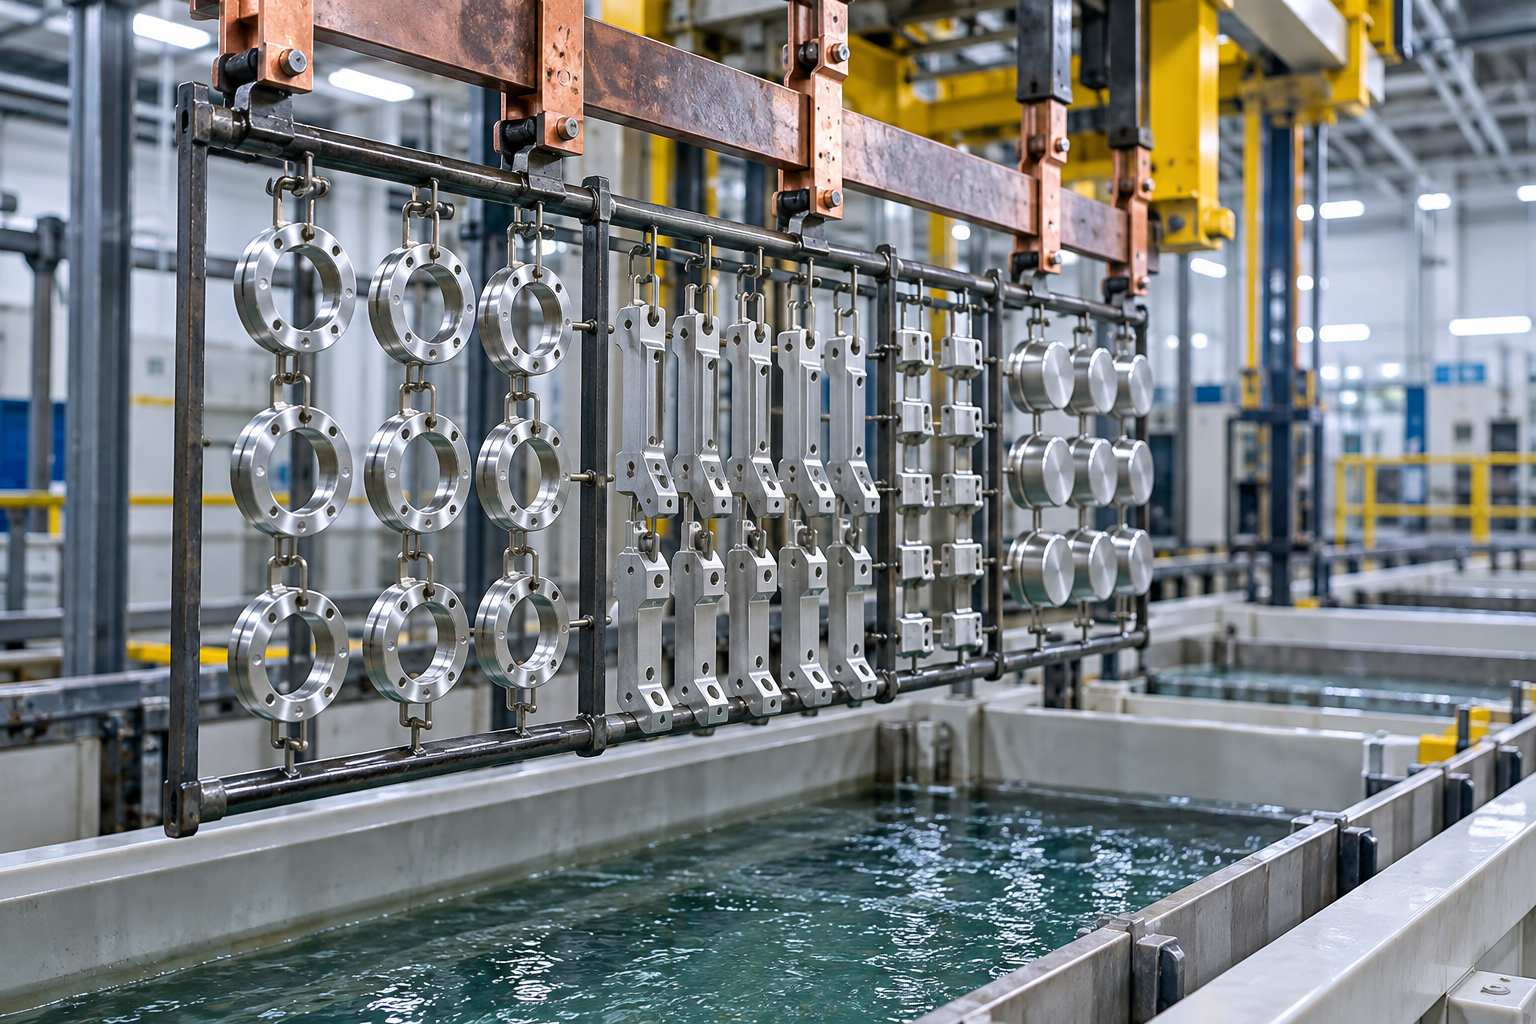
Rack Contact Design for Stable Current Distribution in Electroplating is not a one-variable purchasing decision. In automatic electroplating and surface-treatment production lines, material choice, equipment settings, operating conditions and downstream construction interact. A specification that lists only a product name or one headline value can leave important risks unresolved. This guide organizes the questions that buyers, engineers and suppliers should review before approving a trial or production order.
The aim is not to prescribe one universal design. Different applications can justify different limits, and final performance often depends on the complete system. Use the following framework to define service conditions, request comparable evidence and validate a representative finished article. Do not treat general guidance as a substitute for project-specific engineering, safety or regulatory review.
Treat the Rack as an Electrical Tool
The rack carries parts, establishes electrical contact and positions surfaces relative to anodes and solution movement. For project teams, this point should be converted into a written requirement rather than left as an informal expectation. Consider normal production, startup, shutdown, cleaning, storage and foreseeable upset conditions, because the most demanding combination may not appear during a short demonstration.
Include total current, part geometry, contact marks, loading density and handling method in the design brief. Ask the supplier to state the method, sample preparation, tolerance, inspection frequency and action taken when a result drifts. When finished-system performance is involved, confirm it with a representative production trial and keep the approved sample and records for later lot comparison.
Size Contacts for Real Operating Conditions
Nominal current capacity is not enough when contact area changes with wear, deposits, spring force or operator loading. The practical risk is that a single laboratory value may not represent production variation, installation details or real operating conditions. Consider normal production, startup, shutdown, cleaning, storage and foreseeable upset conditions, because the most demanding combination may not appear during a short demonstration.
Review current density at contact points, temperature rise, cleaning frequency and the effect of partial contact. Ask the supplier to state the method, sample preparation, tolerance, inspection frequency and action taken when a result drifts. When finished-system performance is involved, confirm it with a representative production trial and keep the approved sample and records for later lot comparison.
Place Contacts With Appearance in Mind
Contact marks and local shielding must be located where they do not compromise critical functional or cosmetic surfaces. A useful specification connects the intended service condition to evidence that both buyer and supplier can review consistently. Consider normal production, startup, shutdown, cleaning, storage and foreseeable upset conditions, because the most demanding combination may not appear during a short demonstration.
Approve contact location on actual drawings and inspect coated samples from several rack positions. Ask the supplier to state the method, sample preparation, tolerance, inspection frequency and action taken when a result drifts. When finished-system performance is involved, confirm it with a representative production trial and keep the approved sample and records for later lot comparison.
Maintain Conductive Surfaces
Coating buildup and chemical residue increase resistance and can create intermittent defects across a production shift. This is also a communication issue: design, purchasing, production and maintenance teams should use the same definitions. Consider normal production, startup, shutdown, cleaning, storage and foreseeable upset conditions, because the most demanding combination may not appear during a short demonstration.
Define stripping, inspection and replacement criteria and make the maintenance method compatible with rack materials. Ask the supplier to state the method, sample preparation, tolerance, inspection frequency and action taken when a result drifts. When finished-system performance is involved, confirm it with a representative production trial and keep the approved sample and records for later lot comparison.
Validate Distribution Across the Load
Parts near anodes, tank edges or solution inlets may plate differently from parts in shielded positions. For project teams, this point should be converted into a written requirement rather than left as an informal expectation. Consider normal production, startup, shutdown, cleaning, storage and foreseeable upset conditions, because the most demanding combination may not appear during a short demonstration.
Map thickness and appearance across a fully loaded rack and adjust shields, thieves, spacing or process settings using trial evidence. Ask the supplier to state the method, sample preparation, tolerance, inspection frequency and action taken when a result drifts. When finished-system performance is involved, confirm it with a representative production trial and keep the approved sample and records for later lot comparison.
Building a Reliable Procurement Brief
A good procurement brief for automatic electroplating and surface-treatment production lines should identify the application, operating envelope, interfaces, required evidence and acceptance process. It should also separate mandatory criteria from preferences. This makes supplier responses easier to compare and prevents an attractive but incomplete data sheet from becoming the only basis for a technical decision.
Before release, review the brief with the people who will process, install, operate and maintain the product or equipment. Resolve ambiguous terms, name the reference standards and agree how deviations will be handled. A small, well-documented trial usually provides more useful evidence than a large order based on assumptions.
Conclusion
Leimeng Plating Equipment recommends matching specifications to the real application and confirming critical points through representative samples or trials. Buyers should evaluate complete-system behavior, process consistency, traceability and maintainability alongside nominal specifications. This disciplined approach supports clearer quotations, smoother approvals and fewer surprises during production or operation without relying on unsupported performance claims.